How to Choose the Right Steam Flow Meter for Your Pipeline?
2026-10-12
Steam is one of the most widely used energy media in industrial applications—and one of the most expensive to produce and distribute. Accurate steam flow measurement directly affects energy cost allocation, process control, and carbon emissions management.
However, steam behaves differently from conventional gases and liquids. Phase changes, the relationship between temperature and pressure, and liquid droplets carried in saturated steam can make flow measurement significantly more complicated. Steam quality, particularly the dryness fraction, is another critical factor that can affect measurement accuracy.
The key to selecting the right steam flow meter is to identify the steam condition first, match the measurement technology to the application, and evaluate accuracy together with the required compensation method.
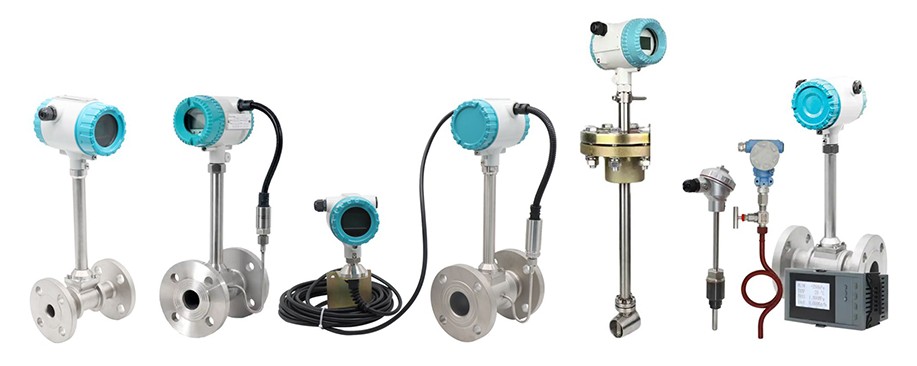
1. Main Types of Steam Flow Meters and Their Accuracy
Different flow meter technologies offer different advantages in steam measurement. The most suitable option depends on operating pressure, temperature, flow range, steam quality, pipe size, installation conditions, and accuracy requirements.
| Flow Meter Type | Typical Accuracy | Key Advantages | Suitable Steam Applications | Main Limitations |
|---|---|---|---|---|
| Vortex Flow Meter | ±1.0% to ±1.5% | No moving parts, relatively low pressure loss (approximately 1/4 to 1/2 that of some differential-pressure installations), wide turndown ratio of 15:1 to 30:1, and potentially low maintenance requirements | Saturated and superheated steam headers, boiler rooms, heat exchange stations, district heating, and industrial process steam | Sensitive to pipeline vibration, requires adequate straight pipe lengths (typically 10–20D upstream and at least 5D downstream), and may have limited performance at low flow velocities |
| Differential Pressure Flow Meter (Orifice Plate/V-Cone) | ±1.0% to ±2.5% | Established technology, suitable for high-temperature and high-pressure applications, relatively simple construction, and competitive initial cost | Power plant main steam, high-pressure superheated steam, and stable, high-flow applications | Higher pressure loss, typically narrower turndown ratio of 3:1 to 5:1, potential impulse-line blockage or condensation issues, and more demanding installation and maintenance |
| Gas Ultrasonic Flow Meter | ±0.5% to ±2% | No moving parts, negligible pressure loss, bidirectional measurement capability, and suitability for large pipelines | Large steam headers of DN300 and above, where the instrument is specifically designed and qualified for steam service, and district heating main pipelines | Wet steam can significantly affect measurement performance; small-diameter installations may be expensive; bubbles and impurities can interfere with some designs |
A Critical Consideration: Steam Condition and Compensation
The first step in steam flow meter selection is to determine whether the application involves saturated steam, superheated steam, or wet steam.
For saturated steam at equilibrium, pressure and temperature are closely related. Depending on the instrument configuration and the required measurement accuracy, a single-parameter compensation method may be sufficient for density calculation. However, insufficient steam dryness can undermine the measurement itself.
Superheated steam requires particular attention because its density depends on both pressure and temperature. Without appropriate pressure and temperature compensation, the calculated density—and therefore the mass flow rate—can deviate significantly from the actual value.
Some reported calculations indicate that pressure-only compensation can produce errors of 6.69%–11.32%, while temperature-only compensation can result in errors of 66.98%–156.50% under certain operating conditions. These figures are condition-dependent rather than universal. For demanding superheated-steam applications, pressure and temperature compensation together are generally essential for reliable mass flow measurement.
2. Five Major Challenges in Steam Measurement and How to Address Them
2.1 High Temperature and High Pressure: Material Selection and Mechanical Design
Steam systems commonly operate above 250°C, and some industrial processes exceed 500°C. The flow meter must be selected according to the maximum operating temperature, pressure, and other process conditions.
Vortex flow meters are available in configurations rated for temperatures up to approximately 450°C and pressure classes up to PN420, depending on the specific model and design. When selecting an instrument, check the pressure rating, sensor construction, body material, and gasket compatibility. Metal spiral-wound gaskets may be suitable for many high-temperature applications, but the final selection must match the actual service conditions.
For superheated steam operating at 300–420°C or higher, the instrument must have adequate temperature and pressure margins. Do not select a meter based solely on its nominal size or stated maximum temperature; confirm that the complete assembly is rated for the intended operating conditions.
For ultra-high-pressure superheated steam above 10 MPa, differential-pressure technologies such as orifice plates and flow nozzles can be particularly suitable because of their established use in high-pressure steam systems.
2.2 Steam Dryness: Why Wet Steam Can Undermine Measurement Accuracy
Liquid water droplets entrained in saturated steam can significantly affect flow measurement. The dryness fraction represents the mass proportion of vapor in a saturated liquid-vapor mixture. A lower dryness fraction means more liquid water is present.
Some reported data indicate that steam with a dryness fraction of 0.90 may increase the measurement error of a vortex flow meter by approximately 5% and that of a differential-pressure flow meter by approximately 8%. Actual errors depend on the instrument design, flow conditions, and installation.
For wet steam with a dryness fraction below 0.85, installing a steam-water separator and improving drainage should be considered before selecting the meter. Differential-pressure measurement may be an option for certain applications, but it is not immune to wet-steam errors.
Vortex flow meters may experience signal degradation or distorted measurements when liquid water accumulates in the pipeline. Install suitable steam traps and drainage points upstream, and ensure that condensate does not accumulate around the meter.
Important: A separator and steam traps can improve steam quality, but they do not automatically guarantee accurate measurement. The remaining liquid content and the selected meter's capabilities must still be evaluated.
2.3 Condensate and Two-Phase Flow: Pipeline Design and Drainage Matter
Steam leaving a boiler is often saturated or slightly superheated. During long-distance transportation, heat loss can cause condensation.
Condensate accumulating at low points in a steam pipeline can create water hammer, potentially damaging the flow meter, pipeline, and associated equipment.
To reduce these risks:
-
Provide adequate drainage points and correctly sized steam traps throughout the steam distribution system.
-
Avoid installing the flow meter at the lowest point of the pipeline, where condensate may accumulate.
-
Ensure that the pipeline layout supports effective condensate removal.
-
For differential-pressure installations, design the impulse lines according to the applicable steam measurement practice. Condensate-filled impulse lines or appropriate sealing arrangements may be required to protect the differential-pressure transmitter from direct exposure to high-temperature steam.
Proper drainage and installation are essential for measurement stability, equipment protection, and long-term reliability.
2.4 Large Flow Variations: Turndown Ratio Determines Low-Load Performance
Steam demand can vary considerably with production schedules, seasonal changes, and equipment operating conditions. During nighttime operation or summer shutdown periods, the actual flow may fall to only 10%–20% of the design value.
Vortex flow meters commonly offer turndown ratios of approximately 15:1 to 30:1, depending on the model and operating conditions. However, their performance at low flow rates depends on the minimum measurable velocity, steam density, sensor design, and pipeline conditions.
Do not select a flow meter based only on the existing pipe diameter. Instead, calculate the expected minimum, normal, and maximum flow rates.
Where the normal operating flow is much lower than the meter's effective measurement range, a properly engineered reduced-bore installation may improve low-flow performance. The solution must still satisfy pressure loss, velocity, and installation requirements.
2.5 Pipeline Vibration: A Key Limitation of Vortex Flow Meters
Vortex flow meters determine flow velocity by detecting the frequency of vortices generated by a bluff body. Mechanical pipeline vibration can introduce interference signals at frequencies close to the vortex signal, potentially causing false counts, unstable readings, or zero-point drift.
Vibration risks are particularly important near pumps, compressors, control valves, and pressure-reducing valves.
Where necessary, install appropriate pipe supports and vibration-isolation measures. Supporting the pipeline approximately 2D upstream and downstream of the meter may be considered as an initial engineering reference, but the final support arrangement should follow the manufacturer's installation recommendations and site-specific vibration assessment.
If vibration cannot be adequately controlled, consider a vibration-resistant vortex model or evaluate an alternative technology, such as differential-pressure measurement.
3. Five Key Factors for Selecting a Steam Flow Meter
3.1 Identify the Steam Type
Saturated steam
Saturated steam has a defined pressure-temperature relationship under equilibrium conditions. Pressure compensation is commonly used for density calculation, although the appropriate approach depends on the application and required accuracy.
Steam dryness remains critical. If excessive condensate is present, resolve the drainage and steam separation issues before relying on the meter reading.
Superheated steam
Superheated steam requires accurate density calculation based on pressure and temperature. For mass flow measurement, use a suitable pressure and temperature compensation arrangement and an appropriate steam-property calculation method.
Vortex and differential-pressure meters are common options. Ultrasonic technology should only be considered where the specific instrument is designed and validated for the relevant steam conditions.
Wet steam
When the dryness fraction falls below 0.85, consider a steam-water separator, effective condensate drainage, and a measurement technology suitable for the actual two-phase conditions. Differential-pressure measurement may be considered for some applications, but no conventional single-phase flow meter should be assumed to deliver accurate results in uncontrolled wet-steam conditions.
3.2 Collect the Complete Operating Parameters
Before selecting a steam flow meter, confirm the following information:
-
Minimum, normal, and maximum mass flow rates in kg/h
-
Normal, minimum, and maximum operating pressure
-
Normal, minimum, and maximum steam temperature
-
Nominal pipe diameter (DN) and pipeline material
-
Available upstream and downstream straight pipe lengths
-
Locations of pumps, compressors, valves, and other vibration sources
-
Hazardous-area classification and required explosion protection
-
Required output signals, such as 4–20 mA, pulse, RS485, or HART
-
Whether the measurement is used for internal energy management or commercial billing
The most important point is to size the instrument according to the actual flow range rather than simply matching the existing pipe diameter.
3.3 Match Accuracy Requirements with the Compensation Method
The required accuracy depends on how the measurement data will be used.
Commercial billing and energy cost allocation
A vortex flow meter with appropriate temperature and pressure compensation may be suitable for many steam billing applications. Accuracy requirements, verification procedures, and legal metrology obligations must be confirmed with the relevant local authority and project specifications.
For demanding billing applications, consider a nominal accuracy class of 1.0 where appropriate, together with the required verification documentation and calibration arrangements.
Internal energy accounting and process monitoring
Vortex or differential-pressure flow meters with typical accuracy in the range of ±1.0% to ±1.5% may be adequate for many applications, provided the meter is correctly sized, installed, and compensated.
Large-diameter headers and district heating networks
Ultrasonic flow meters may offer accuracy of approximately ±0.5% to ±1% of reading in suitable applications. Confirm that the selected model is specifically qualified for steam service and the actual operating conditions.
Understand the accuracy specification
Always distinguish between accuracy expressed as a percentage of reading and accuracy expressed as a percentage of full scale. These specifications behave differently at low flow rates. For the same numerical percentage, a full-scale-based error can represent a much larger proportion of the actual reading at low flow.
3.4 Evaluate the Installation Environment
Adequate straight pipe length helps stabilize the flow profile and improve measurement reliability.
The following values are general starting points, not universal requirements:
| Flow Meter Type | Typical Upstream Straight Length | Typical Downstream Straight Length |
|---|---|---|
| Vortex flow meter | At least 10–15D; 15–20D or more may be required after certain upstream disturbances | At least 5D |
| Differential-pressure flow meter | Approximately 10–20D, depending on the primary element and upstream disturbance | Approximately 5–10D, depending on the installation |
| Ultrasonic flow meter | Approximately 15D or more, depending on the meter design and flow disturbance | Approximately 5D or more, depending on the meter design |
Here, D represents the internal pipe diameter. Always follow the manufacturer's installation instructions and the applicable standards for the selected instrument.
Vortex flow meters should be installed away from significant vibration sources wherever possible. Steam pipelines must also have adequate drainage and appropriate installation geometry to prevent condensate accumulation.
3.5 Consider Maintenance Requirements and Total Cost of Ownership
Vortex flow meters: With no moving parts, they can offer low maintenance requirements over long operating periods. Actual maintenance intervals depend on the application and operating environment.
Differential-pressure flow meters: Impulse lines may require inspection and cleaning, while orifice plates and other primary elements need periodic inspection for wear, fouling, or damage.
Ultrasonic flow meters: These meters generally have no moving parts and can require relatively little routine maintenance. However, sensor construction, temperature exposure, and environmental conditions must be considered when evaluating long-term reliability.
The purchase price is only one part of the cost. Installation, pressure loss, downtime, calibration, and long-term maintenance should all be included in the selection decision.
4. Recommended Steam Flow Meter Solutions from Aister Instrument
Shanghai Aister Instrument has developed steam flow measurement solutions for applications involving high temperatures, elevated pressures, condensate formation, and potential vibration interference.
Its steam measurement product range is centered on the ATLU vortex flow meter series. According to the manufacturer's product information, the range includes explosion-protected configurations and factory flow calibration capabilities, with applications in district heating, industrial process steam, and boiler-room energy monitoring.
The final model should always be selected according to the actual operating conditions, required accuracy, applicable certification requirements, and installation constraints.
4.1 ATLU Integrated Temperature and Pressure Compensation Vortex Flow Meter
The ATLU series is one of Aister Instrument's principal solutions for steam measurement. Based on the Kármán vortex principle, it uses a piezoelectric sensing design to detect vortex frequency.
Key technical specifications
| Parameter | Specification |
|---|---|
| Nominal Diameter | DN15–DN300 for flanged models; insertion designs available for larger pipes |
| Accuracy | ±1.0% for liquids and ±1.5% for gases/steam in inline configurations; ±2.5% for insertion configurations |
| Turndown Ratio | Up to 20:1 |
| Medium Temperature | -40°C to +350°C |
| Operating Pressure | 1.6, 2.5, 4.0, or 6.4 MPa, depending on configuration |
| Output Signals | Pulse and 4–20 mA; RS485 and HART available as options |
| Protection Rating | IP67 |
| Connection Options | Flanged, wafer, insertion, and clamp connections |
| Temperature and Pressure Compensation | Optional integrated temperature and pressure sensors for automatic density correction |
The ATLU series can be configured with integrated temperature and pressure sensors to calculate density internally and provide compensated flow outputs. Depending on the selected configuration, the system can reduce the need for separate compensation instruments and simplify installation.
Available configurations include flanged, wafer, insertion, and clamp-connected designs, covering a range of pipe sizes and retrofit requirements.
Potential applications include:
-
District heating steam headers with pipe sizes of DN150–DN300
-
Primary steam measurement at heat exchange stations with pipe sizes of DN50–DN150
-
Industrial steam measurement where flow data are used for energy allocation or commercial settlement
Confirm the required output variable, compensation configuration, and applicable accuracy specification before ordering.
4.2 ATLU Corrosion-Resistant and Explosion-Protected Vortex Flow Meter
For chemical plants and petrochemical facilities, the ATLU series can be configured for applications that require corrosion resistance and explosion protection.
According to the specified product configuration, the meter offers accuracy classes of 1.0 or 1.5, operating pressure options from 1.6 to 6.4 MPa, and different temperature ranges:
-
Standard version: -40°C to +150°C
-
Medium-temperature version: -40°C to +250°C
-
High-temperature version: -40°C to +350°C
The specified explosion-protection marking is Ex d IIC T6. Suitability must be confirmed against the actual hazardous-area classification, ambient temperature, process temperature, and the certificate applicable to the exact model.
For corrosive service, material options such as 316L stainless steel or PTFE lining may be considered where technically appropriate. Material compatibility must be verified against the steam conditions and any contaminants present.
Integrated temperature and pressure compensation is available in selected configurations for compensated flow measurement.
4.3 High-Temperature Remote-Mounted Vortex Flow Meter
For high-temperature applications in power generation and metallurgy, Aister offers a remote-mounted vortex flow meter configuration.
The specified sensor temperature capability reaches up to 450°C, with the converter installed separately from the sensor. Separating the electronics from the high-temperature measurement point helps reduce their exposure to heat.
This configuration may be suitable for steam applications operating between 350°C and 450°C, subject to the model's pressure rating and other installation limits.
For applications exceeding the specified temperature rating, such as certain power plant main-steam systems, a suitably rated differential-pressure solution or another qualified measurement technology should be evaluated.
Aister Steam Flow Meter Selection Quick Reference
| Application | Recommended Solution | Key Selection Considerations |
|---|---|---|
| District heating steam header, DN150–DN300 | ATLU flanged vortex meter with integrated temperature and pressure compensation | Appropriate accuracy class, RS485 communication if required, and continuous-operation suitability |
| Saturated steam at a heat exchange station, DN50–DN150 | ATLU flanged vortex meter | Appropriate pressure rating, temperature and pressure compensation as required, and flange compatibility |
| Industrial steam commercial settlement | ATLU vortex meter with suitable accuracy and verification documentation | Confirm legal metrology requirements, calibration arrangements, and applicable measurement certification |
| Steam in hazardous chemical plant areas | ATLU corrosion-resistant, explosion-protected vortex meter | Applicable explosion-protection certification, pressure and temperature ratings, and material compatibility |
| High-temperature superheated steam in power generation or metallurgy | High-temperature remote-mounted vortex meter, where rated, or a suitable differential-pressure meter | Confirm maximum temperature and pressure, installation conditions, and compensation requirements |
| Large steam header, DN300 and above | ATLU insertion vortex meter, where suitable | Confirm the available diameter range, insertion design, pressure requirements, and whether online installation is permitted |
For large pipelines, the manufacturer specifies insertion configurations for applications up to DN2000. The maximum diameter, pressure conditions, and whether hot tapping or online installation is feasible must be confirmed for the selected model.
5. Steam Flow Meter Recommendations for Typical Applications
Scenario A: District Heating Steam Header
Operating conditions: DN200 pipeline, saturated steam, pressure of 1.6 MPa, and significant flow fluctuations.
A possible choice is the Aister ATLU integrated temperature and pressure compensation vortex flow meter in a DN200 flanged configuration.
For applications requiring an accuracy class of 1.0, confirm that the selected model and complete measurement system meet the project specification. RS485 communication can be used to transmit measurement data to a supervisory or dispatching system when supported by the selected configuration.
Pay particular attention to vibration from nearby pumps, traffic, or other mechanical sources. Appropriate pipe supports and vibration-control measures may be required.
During low-demand periods, such as summer operation, the actual flow may fall below the meter's effective measurement range. Check the minimum expected flow before finalizing the nominal diameter. A properly designed reduced-bore installation may be worth evaluating.
Scenario B: Chemical Plant Steam Heating Branch
Operating conditions: DN80 pipeline, superheated steam, temperature of 300°C, and pressure of 1.0 MPa.
A suitable candidate may be an ATLU explosion-protected vortex flow meter with a compatible 316L stainless steel body and an appropriate temperature rating.
The specified Ex d IIC T6 marking must be verified against the actual certificate and hazardous-area requirements before purchase.
Because the medium is superheated steam, density calculation should use both pressure and temperature. An integrated compensation arrangement or a suitable external pressure and temperature measurement system can be used, depending on the selected configuration.
Using pressure-only or temperature-only compensation without verifying its suitability may introduce significant mass flow errors.
Scenario C: Clean Steam for Food Processing CIP/SIP
Operating conditions: DN50 pipeline and low-pressure saturated steam at 0.5 MPa.
An ATLU flanged vortex flow meter may be considered where the operating conditions and required accuracy match the product specifications.
Ensure that the pipeline is adequately drained and that condensate does not enter or accumulate around the meter. Where vibration is low and sufficient straight pipe length is available, a vortex flow meter may provide a practical balance between measurement performance and installation cost.
For clean-steam applications, also verify the required hygienic design, wetted-material compatibility, and cleaning or sterilization requirements. A standard industrial vortex meter should not automatically be assumed to meet sanitary or pharmaceutical requirements.
Scenario D: High-Temperature, High-Pressure Superheated Steam in a Power Plant
Operating conditions: DN250 pipeline, temperature of 540°C, and pressure of 14 MPa.
The standard Aister high-temperature remote-mounted vortex configuration described above has a specified sensor temperature limit of 450°C. It therefore cannot be selected for a 540°C application unless a separate, specifically rated model is available and verified.
A differential-pressure flow meter or another measurement system rated for the actual pressure and temperature should be evaluated.
The system may require appropriately rated pressure and temperature instruments, such as redundant Pt100 resistance temperature detectors and a pressure transmitter, together with a suitable steam-property calculation method.
The final design must consider pressure containment, material selection, installation requirements, and the applicable power plant standards. Where space is limited, a reduced-bore arrangement should only be adopted after checking its effect on velocity, pressure loss, and measurement performance.
6. Common Steam Flow Meter Selection Mistakes to Avoid
Mistake 1: Using Only One Compensation Parameter for Superheated Steam
The density of superheated steam depends on both pressure and temperature. Relying on only one parameter can cause substantial density calculation errors.
For demanding superheated-steam applications, use an appropriate pressure and temperature compensation arrangement and a validated steam-property calculation method, such as IAPWS-IF97 where applicable.
Mistake 2: Measuring Wet Steam Without Addressing Condensate
No conventional single-phase flow meter should be assumed to provide accurate results when the steam contains uncontrolled amounts of liquid water.
For wet-steam conditions, particularly when the dryness fraction is below 0.85, first evaluate steam separation, drainage, steam trap performance, and insulation. Then select a measurement technology suitable for the remaining operating conditions.
Mistake 3: Selecting a Vortex Flow Meter Based Only on Pipe Diameter
Choosing a vortex flow meter solely because its nominal diameter matches the existing pipeline is a common cause of poor low-flow performance.
The meter may operate below its effective measurement limit during nighttime or low-production periods.
Instead, calculate the minimum, normal, and maximum flow rates before selecting the meter size. A properly engineered reduced-bore installation can sometimes improve the usable measurement range.
Mistake 4: Ignoring Pipeline Vibration
Mechanical vibration near pumps, compressors, control valves, and pressure-reducing valves can interfere with vortex frequency detection and produce unstable readings.
Assess the vibration environment before installation. Add suitable pipe supports and vibration-control measures where necessary. If the interference cannot be resolved, consider relocating the meter or evaluating a different measurement technology.
Mistake 5: Using a Meter for Commercial Settlement Without the Required Verification
Commercial steam measurement may be subject to local legal metrology rules, contract requirements, and verification procedures.
Before ordering, confirm the required accuracy class, calibration documentation, and any applicable metrological approvals with the customer and relevant authority.
An annual verification or calibration interval may be specified by a contract or local regulation, but a 12-month interval should not be treated as a universal requirement for every steam installation. Aister ATLU configurations can be supplied with factory flow calibration where available; confirm the calibration scope and traceability documentation for the exact order.
Conclusion: Select the Steam Flow Meter According to the Actual Operating Conditions
Choosing a high-accuracy steam flow meter involves more than comparing accuracy specifications or matching the nominal pipe diameter. Steam condition, dryness fraction, pressure, temperature, flow variation, vibration, installation space, and compensation method all affect the final measurement result.
Vortex flow meters are practical options for many saturated-steam and superheated-steam applications when the flow conditions, installation, and compensation system are suitable. Differential-pressure meters remain important for many high-pressure steam applications, while ultrasonic technology should be selected only when the specific instrument is qualified for the intended service.
Aister Instrument offers ATLU vortex flow meter configurations for a range of industrial steam applications, including integrated temperature and pressure compensation, explosion-protected designs, and remote-mounted high-temperature configurations.
Before selecting a model, provide the minimum, normal, and maximum flow rates, operating pressure and temperature, pipe diameter, steam type, required output signals, and installation conditions. These details allow the measurement solution to be matched more accurately to the actual process.
Contact Aister Instrument to discuss your steam flow measurement requirements and identify a suitable flow meter configuration for your application.
Share To:
Next Post:
News
- Why is the thermal gas mass flowmeter not affected by pressure strength and temperature?
- What to do when a thermal gas mass flow meter fails?
- How are thermal gas mass flow meters used? What are the applications?
- Under what circumstances is the gas measurement need to be regulated compensated vortex flowmeter
- Why Is The Aister Thermal Gas Mass Flowmeter So Popular ?
- Gas turbine flowmeter manufacturers explain their main advantages in measurement
- Gas turbine flowmeter manufacturer Aister instrument field experience summary
- Aister Instrument Empowerment Conference